Showing posts with label Deburring. Show all posts

Sunday, March 17, 2019

Round 3 - Making a Template of the Removeable Section of the LE

yup - another round of lousy weather, delays - yada yada yada has yielded very little work on the project in over a month. It's been way too cold to work in the garage, and we just experienced a lovely thing that some moron decided to call a bomb cyclone several days ago that resulted in our first real blizzard in the Denver area in a good long while.

Anyway, to pick up where I left off, I had one last chapter in this whole removeable section fabrication  to cover before I move on to what I was finally able to get done today. After finally getting a part sized, trimmed, fitted, and drilled with correctly positioned mounting holes to #30, I now needed to make a template. The problem was that the part that I was finally happy with had been fitted to the LE, and as a result it was now slightly curved, and this presented some problems with trying to fabricate a new plat piece of metal out of another slight curved piece of metal.

As a long story short, I decided that I could probably use some weights to re-flatten the "good" part just enough for me to draw a matching pattern onto a piece of .025 flat metal again, just as I had done to make the part that I have finally deemed "good." the big deal about all this was trying to take advantage of the precut "factory" edges of the new metal, because their cutting machines and processes are much more accurate than mine. I wanted to do this so that at least two of the edges would be absolutely straight. This minimizes any additional work I need to do to trim and shape the other two edges to get a good fit. The other issue is to ensure that the holes are drilled in the correct spots, and that the curves in each of the four corners are radiused correctly.

At the end of it all, it made me really appreciate metal parts that are precision cut, punched, and fabricated by precision tools. What follows is a series of pics showing how I went about making the template from which I would be able to make as many more of these as desired. First up was a process of taking the now partially bent "good" part and setting into position against the two good edges of the .025 sheet using some cleco clamps and my bucket of very heavy #40 clecoes. This did a pretty good job of flattening the part back down so that I could trace the edges onto the new sheet and also match drill the holes around the perimeter.
This turned into a very involved exercise of precise clamping and drilling, moving things around as necessary and re-clamping again. I used the wood from my drill board to match drill the holes and then cleco both parts directly onto the drill board.
After it was all done the holes were deburred and the top and bottom and edges were marked, and it was cut from the sheet using either shears or my Dremel tool cutoff wheel. The problem with this next one is that I ended up trimming to much material away from the corners and edges and so this one did not fit very well and I had to make yet another one.
So I ended up making another one where I intentionally added a bit more material on the edges to ensure that I would not come up short. So after making 3 more of these crazy things I finally ended up with a keeper that I could use for flat template that could be used to accurately make more of them as necessary. Trimming the corners to have just the right radius is also a challenge. 

Here are some pics of the horrible trimming job I did tht forced me to have to make yet another template:


Yeah they are blurry but you can still see how bad the gaps are. This was just not acceptable so I started over.


SO now we can fast forward to today. The problem was that I could  NOT continue with anything on the LE until had this template made correctly, because the next step in this process was to upsize each of the #30 holes in the good part to #19 for the #8 dimples and screws that will be inserted into them to attach the part to the subskin. 

So with a "good enough" template now completed, I reattached the good part to the LE and then re-clecoed the LE skin securely onto the wing spar to make certain that everything was in the proper position  before drilling the holes. Then I took the #19 drill bit and started upsizing each of the #30 holes in the removeable section as well as the subskin underneath. I used the black colored clecoes to secure the section to the subskin as I went. I had 20 holes to upsize and only 10 clecoes, so I had to be creative about how I did this. I upsized all the holes on the top side of the LE first, followed by the bottom holes. Then I used my deburring bit and my edge deburring tool to ensure that the holes were very clean and smooth, just as I had done for the tank attach holes long ago, so that the #8 dimples would not have any cracks in them. 

Here are pics of the top and bottom sides after the holes had been upsized and the removable section was removed. the #40 holes for the rivets that will hold each nut plate were already drilled and dimpled long ago, so this exercise is just for the 20 (10 top and 10 bottom) center screw holes.
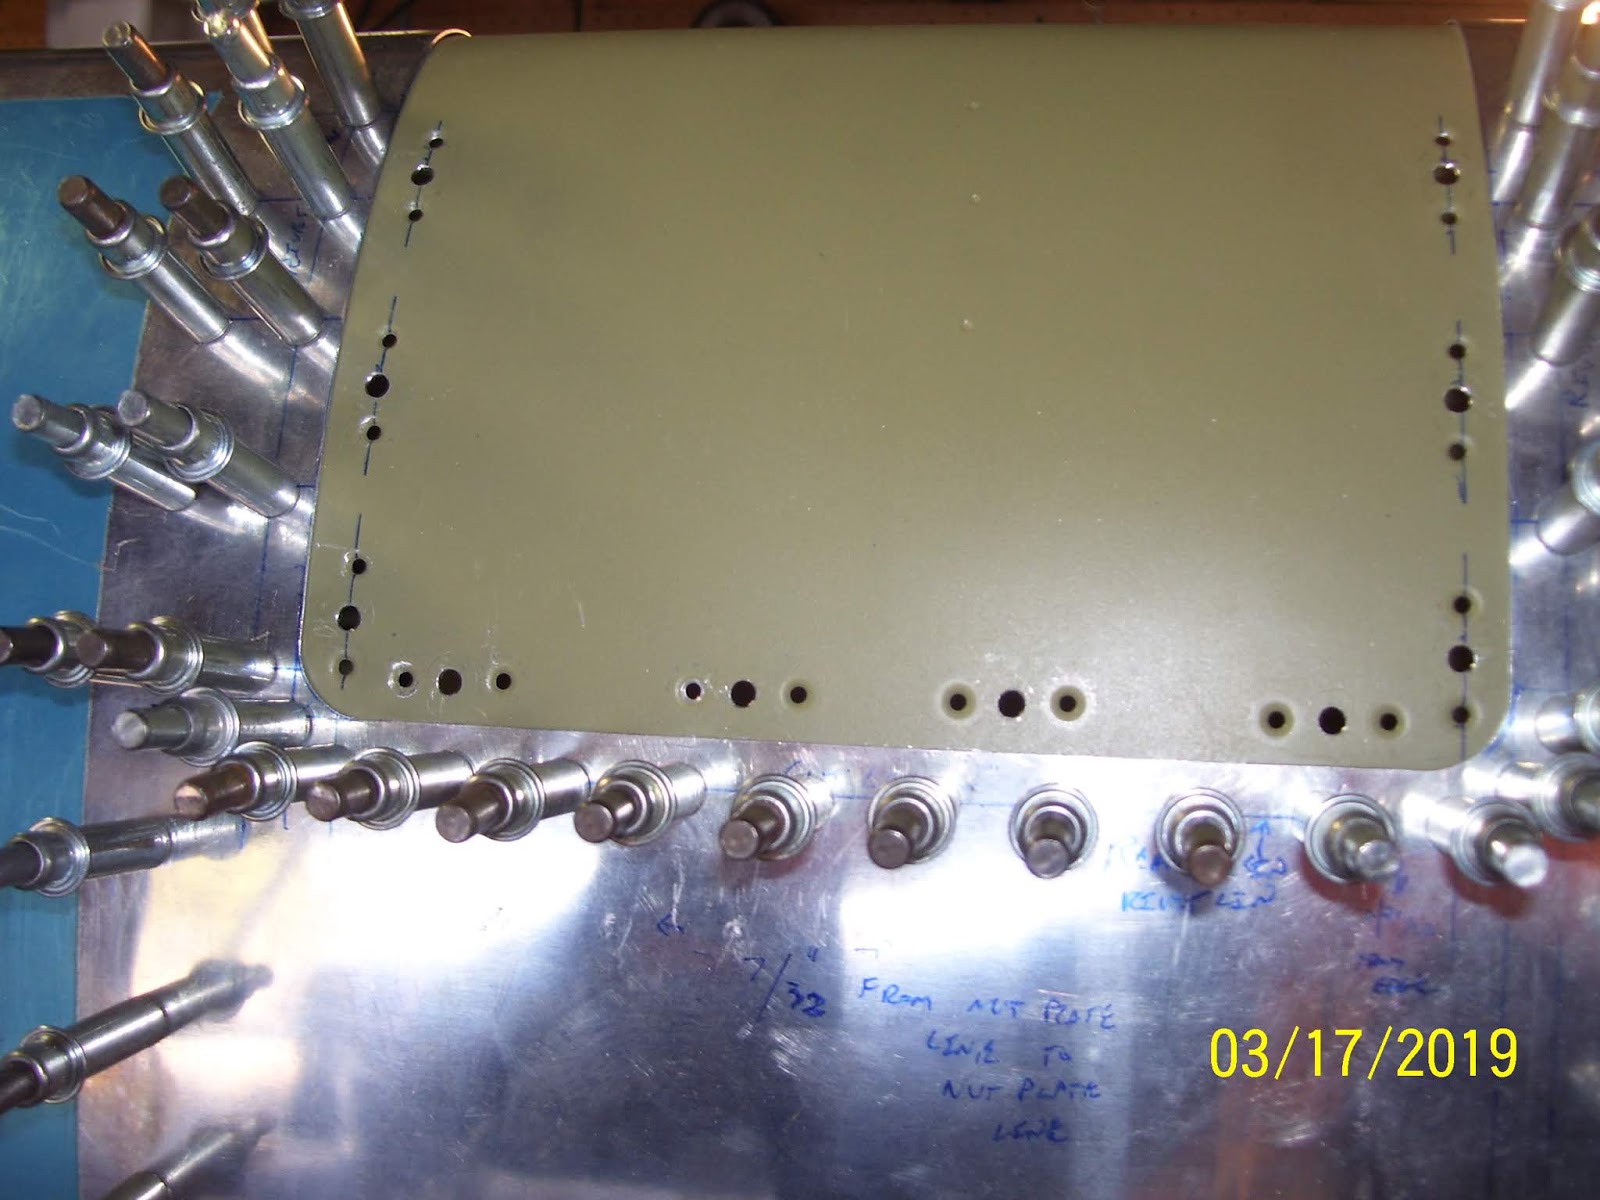
And here are the top and bottom side pics of the removeable section after I dimpled all the holes on both sides

I was glad that all the dimples seem to have come out well. While setting the dimples in the removeable section was relatively easy since it is not bent very much, forming the #8 dimples on the subskin turned out to be yet another interesting exercise to set these dimples. It required using both hands and my head to position each hole over the male dimple die in my C Frame and keep the metal away from the ram, so that I could use the ball peen hammer to set each dimple by whacking it a few times. Just as when I previously set the dimples for the tank attach nutplates on the subskin several months ago, the holes nearest the front of the subskin closest to the bend were the hardest to set.
 
With the dimples on the removeable section done the next step was to remove the LE from the wing spar for what I hope is the absolute FINAL time before I permanently affix it to the wing spar, and remove the subskin so that I could set those dimples as described above. This also went reasonably well, despite the awkward contortions of my hands and head required to set them.
 

I also took a pic of the new "final" flat template, and the label I wrote on it to ensure that I would be able to tell months from now that I would be able to to tell which template is the "good" one as I proceed to create the same thing for the right wing LE. However since I doubt that I will end up with everything sized exactly the same on the right wing, I think I will end up making a customer one for the right wing as well, when the time comes.


With all the #8 dimples done, it was time to cleco the K1100-8 nut plates in place on the subskin s I could start riveting those in place. I did not quite get to that today, so that will be my next task that I will hopefully complete next week. Here is the subskin with all the nut plates clecoed into position:

I cant believe that I am finally at a point where I can start to assemble the left wing LE for the final time once these nut plates have been riveted. That's all for tonight. Hopefully much more progress next week.

Saturday, December 15, 2018

Finished the file folder template, match drilled the #30 screw holes, Transfered the template to the metal

A productive day in the shop today, even though I still don't have much to show for it. I decided to prepare a new file folder using the same measurements as before - 11.75 inches long and 7 13/16 inches wide, since the first one got trimmed to the point that it was no longer a very good match. This time I used a pencil with a very fine point for all the measurements, and I was a bit more precise in my measurements and line drawing, etc. The new file folder template came out pretty good, and was a precise match for the space on the top side of the LE. However, when I taped it all down, I was coming up a bit short on the rear edge of the bottom side of the template. But side-to-side and in the corners everything seemed to be aligned pretty well. I did not worry too much about the short length issue because I knew that the bending of the metal will stretch it just a bit, and I am also going to cut the metal a bit larger than the template, and then scotch brite the edges and sand it  down to the precise fit that I need. SO the edges will be exactly how I need them when it is all said and done. Here is the new template re-taped in place on the top side of the LE:
And next is the bottom side. You can see the gap on the bottom left edge near the corner. 
You can also see some of the screw holes that I have "hand drilled" by using a #30 drill bit and my hands and fingers to align it from the inside of the LE through the outer rib, locating the #30 drilled holes in the subskin, and then turning the drill bit just enough to poke the hole through the file folder template. Here is the view of how I did this from the inside. it wasn't too difficult to locate and drill most of the holes, but the last 2 or 3 tested my creative ability to contort my arms, hands, fingers, and body to get the drill bit into the correct holes.
Of course when I drilled the hole through the template  aligned the drill bit as best I could so that it was going straight through the hole in the subskin, which is not the way it is positioned left free-standing through the hole so I could take the picture.. This actually turned out better than I thought it would, and seemed to result in all the holes being properly transferred to the template.

Here is a closeup of what it looks like when the drill bit poked through the file folder template. I used my finger on one hand to apply opposing force on the paper template from the outside, while I used my fingers on my other hand to turn the drill bit from the inside - quite the parlor trick if I do say so myself.
I continued this process until all the screw holes in the subskin were transferred to the template, then I removed the template frome the LE to continue with the rest of the  steps to transfer the shape and hole locations to the .025 T3 2024 aluminum sheet that I had purchased from Vans long ago.
Next I performed yet another not-quite-so-orthodox procedure to transfer the screw holes to the aluminum sheet as shown below. I used the hand-held drill bit once again after taping the template to the aluminum sheet to "mark" the metal through each of the template's screw holes to drill a small amount of material to mark the locations. I also aligned two of the outer edges of the metal with two of the edges of the template, to reduce the amount of work required to cut the part out of the metal by only needing to cut along two of the 4 edges of the part. I did check the metal first to ensure that the two existing edges were square and straight with each other.
All the screw holes locations were marked after I removed the template from the aluminum sheet:
So far so good. I removed enough material with the drill bit to ensure that it would find its center once I was ready to actually drill each hole. I should also mention that the grain of the metal needed to be aligned similar to the rest of the LE skin, so the orientation of the grain, which parallels the magenta printed info on the sheet, was important to note while positioning the template on the metal sheet. You also have to make sure yo specify how you want it cut when you order it from Vans, so specifying the grain direction should always be done, in addition to the other dimensions and the thickness.

Next was setting the sheet up on the drill boards, clamping everything down, and final drilling all the screw holes to #30. Once I know that this is working out well, the #30 holes in this part and in the subskin will be final drilled to #19, and dimpled for the #8 screws that will be inserted in these holes to secure it to the subskin.

I drilled the holes without the template in place with the protective vinyl covering still in place, clecoing the metal to the drill board as I went. Then I removed the vinyl covering from the metal, deburred the holes on both sides of the sheet, and clecoed the template back onto the metal so that I could redraw the outline of the edges again on bare metal. Previously the lines were drawn on the vinyl covering, so when that got removed, I had to redraw the edges again on the bare metal. Here is the template clecoed onto the metal sheet and the drill board so I could redraw the edges on the metal sheet.
And here is a final shot of the metal with all the #30 holes drilled and deburred, and the vinyl removed, and the lines redrawn. Next steps for tomorrow will be to cut out the part from the metal, trim down the edges, and start form fitting and trimming the part until it fits nicely into the cutout on the LE skin. Before I do that, however, I may decide to go ahead and make another metal part with the edge dimensions but no screw holes. The real trick to this is going to be if the screw holes are in the exact position that is needed to ensure that the part lies completely flush and tight with the rest of the LE skin. If it does not I will have to reposition the screw holes a bit. SO this may take 2 or 3 or more iterations before I have it exactly right.


If the holes are right and the fit is right, the next step is to cleco it all in place and final drill the #30 holes to #19, debur and dimple them in the part and the subskin, which of course also means removing and disassembling the LE once again. Getting there (I hope).

KPR


Monday, December 10, 2018

Subskin prep - Drilled and Dimpled Remaining nut plate rivet attach holes and Reassembled the LE

Today was a busy day at the factory, but for the amount of progress I made today you would probably not believe me. I finished sanding the edges of the cutout section of the LE skin smooth and straight, and used the combination of my pneumatic rivet squeezer and C-Frame tools to dimple all remaining #40 nut plate rivet attach holes on the subskin. I had to switch from my flange yoke to the standard 3 inch yoke to be able to reach all the rivet holes along each side of the subskin, and this worked out nicely. I had to use the C-Frame to reach most of the rear-most rivet holes on both sides of the subskin, and this also worked out well.

Unfortunately I had to use the #30 cleco method to secure the nut plate to the subskin so that I could align and drill the holes for each nutplate on the top side of the subskin, just as I had previously done on the bottom side. Just as before, I had trouble keeping the line of rivet holes in alignment with other straight edges, and some of them got a bit slanted. As I stated before, these holes are just for the rivets that attach each nut plate to the subskin, so the MOST important hole is actually the center hole where the screw will be inserted, and not the rivet holes.

I used the same technique to mark the alignment of the rivet holes on the top as I did  on the bottom, by placing a straight edge along the center line of each #30 screw hole and drawing short lines on either side of each hole that I used to align the rivet holes of the nutplate after it was clecoed to the subskin through the screw hole.


I drew the lines along the sides on the outer side of the skin, and drew the lines for rear nut plate holes on the inside of the skin, just as before. As shown from the pic above, I also came up with a different clamping and prep method of drilling these rivet holes. This time I really did not care so much about trying to rig up something so that I could clecoe the nutplate in plate as shown above, and then ensure that I was drilling each rivet hole into a piece of wood. I reasoned that any slag or burr on the holes would be removed by my deburring tool afterward, and so this time I chose NOT to waste a substantial amount of time coming up with ridiculous ways to ensure I could drill each hole into a piece of lousy wood. This worked out fine, except for the slight shifting of the nutplate because the clecoe just does not apply enough force to keep the drill from moving the nut plate around. SO I much prefer using the nut plate jig which prevents this from happening, but since I was not yet ready to drill the #30 hole to a #19 hole yet, which the jig uses as a pilot hole, I could not use the jig tool.

I used my 4x4 clamping blocks to provide some height to allow the cleco mounted from the underside as shown in the next photos to clear the table and saw horse ends, and the next pic shows how I clecoed the first hole after it was drilled, which keeps the second hole from moving around as well, so that both rivet holes are in alignment with each other.


As each set of rivet holes was drilled I detached the nut plate and moved it to the next hole and re-clecoed it in place, and repositioned and reclamped the subskin as necessary to retain some rigitidy in the subskin near the nut plate locations so the drill would not slip or cause the skin to warp and the hole to become mis-aligned. Here is the series of pics as I continued to drill each set of nut plate holes along the sides:


With the sides done it was time to drill the rear nutplate hole. I had to flip the subskin over and reposition and reclamp it once again. I was able to use the edge of the table to help position the skin so that the clecoe underneath butts up against the edge, keeping the skin nice and stiff while drilling.


The last pic above actually shows the holes after I dimpled them. The mot important thing to call attention to here is that I have NOT yet final drilled the screw holes to the proper size because I need to make a template first so that I can fabricate a properly sized part that will replace the cutout section in the skin. I cannot final drill the screw holes to #19 and dimple them for a #8 screw until the template has been created and at least 1 or 2 .025 removeable LE skin sections have been fabricated and fitted in place. To do that I need the screw holes to remain at #30 for now. 

Next I had a bit more cutting, filing and sanding to do on the subskin. A long time ago I had marked the location where the hole for the tie down ring is located by tracing the hole I had already drilled in the LE skin onto the subskin, which, until today, had been covering up that hole. I used the cut off wheel o n the Dremel tool to carefully cut away the metal in this area, staying just OUTSIDE the drawn lines so that  could ensure that the subskin would have enough clearance to screw in the tie down ring. Here is the pic of that after filing, sanding, and rounding all corners was completed:
With most all of the subskin prep work done, it was time to reassemble the LE for what I hope will be the second-to-the-last time before it goes together permanently. the subskin was attached first using all the rivet holes that are not part of a rib flange hole. This gets the subskin in the proper position for the ribs. Then the two inboard-most ribs are clecoed to the subskin and outer LE skin. This process always takes some work because the ribs are a very right fit in this area due to the thickness of the subskin. Again, the goal of all this was to reassemble the LE with the newly cutout section in the skin that exposes the subskin that will be used to attach the removeable LE section.

Here is a series of pics I took to show the fit of the LE and subskin after remounting it all back on the wing spar again. Overall I was pleased, but the problem that I feared and mentioned in a previous post is exactly what I encountered. The outboard are of the cutout section of the LE skin shows a bit of a gap between the subskin and the outer LE skin, whereas the inboard section seems to be draped over the subskin fairly well. This will make fitting the removeable part a bit of  a challenge, but we'll see how that goes. I am not overly concerned about the gap because I think the rib in that area combined with the subskin provides more than enough support to keep the LE from deforming in any way as a result of this gap. In other aircraft designs, such as the Sonex for example, I know that their ribs do not even wrap around the contour of the LE skin. Instead, they stop well short of the very front of the skin so that NONE of the ribs have any rounded contour that wraps around the LE at all, leaving a void between the rib and the very front part of the LE skin.

As long as the shape of the front of the LE skin remains consistent across its entire span I do not see a problem with this. I think this will occur because the rest of the LE outer skin is stressed, so it retains most of its shape due to the tension of the bend that is force-ably wrapped around the top and bottom flanges of each LE rib.

First pic is the top side of the LE with the subskin now showing through:
Next are the inboard and outboard curves of the front of the LE skin showing the gap I mentioned between the LE skin and the subskin  on the outboard section. Both pics are takne from the top side of the LE:


The next set of pics is the same series taken from the bottom side of the LE


And finally 2 pics that show the clearance of the tie down ring hole through both the outer LE skin and the subsin after trimming it away from the subskin. Looks pretty good to me, but I may decide to wien both of the holes a bit to make certain that stresses placed on the ring from high winds etc. will not start contacting the edges of the LE sin in this area. The ring can be screwed in and out with ease.

So this was a day that was very long in the making. I had to wait 2 weeks for it to warm up enough in the garage to get to this point. took about 3 hours or so to do everything described in this post. Next steps are to make the file folder template and fit it to the cutout section of the LE, mark and drill the #30 screw hole locations in the paper template with the LE firmly mounted back on the wing spar, remove the template and use it to trace the new removable section of the LE onto a piece of .025 aluminum. I may decide to go buy some Home Depot grade stuff to practice on until I am certain that I have the outline of the part measured, cut, and formed correctly. My concern now will be what I need to do to make the curved front end of the removeable section match the curvature of the inboard and outboard outer LE skin. Not sure if I will need to apply some shims due to the gap, or if I will be able to pre-stress the removeable section similar to the outer LE skin so that it will retain its shape with the rest of the LE skin. Time will tell on that one.  Hopefully I will be able to get to that point this week since the weather is finally supposed to be warmer.